
 リーダー
You’ve probably seen this disaster unfold before:You spent tens of thousands of dollars engineering a custom mold, fine-tuning the weight, and casting a heavy, high-end Zamak (zinc alloy) perfume cap. Then the shipment arrives.
The logo lacquer flakes off after two scratches.
The electroplated edges turn dark.
The embossed details look like a muddy mess.
That isn’t luxury packaging. That’s an industrial train wreck.
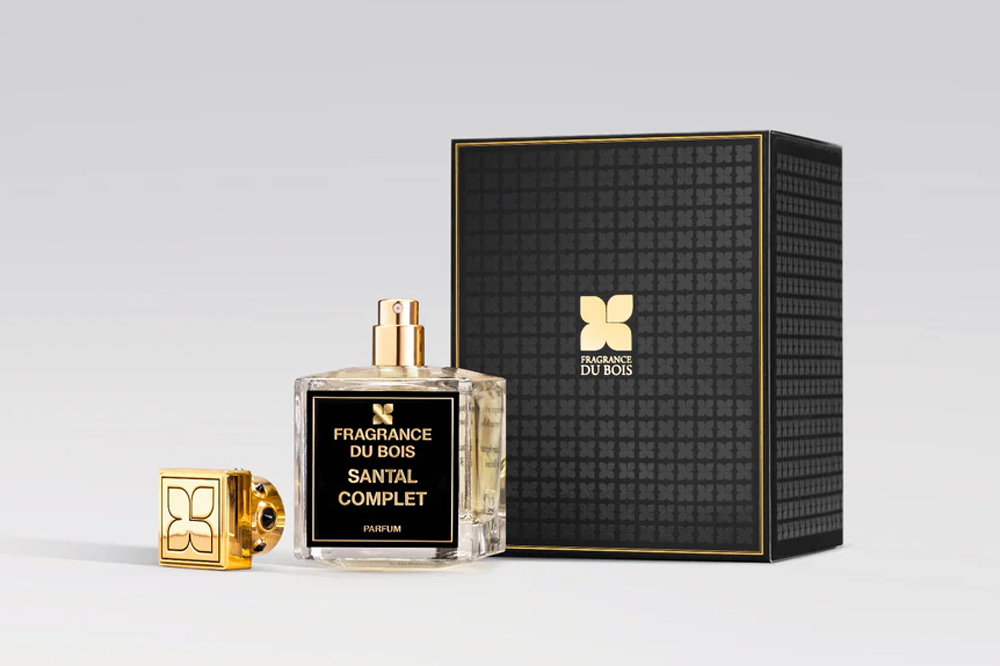
In niche and luxury perfumery, weight creates the initial handfeel. But surface finishing dictates whether your bottle commands $50 or $300 on the shelf.
From a raw sketch to the top shelf at Harrods or Bergdorf Goodman, the real test of a manufacturer isn’t melting zinc alloy into a mold. It’s how precision logos and tactile textures are carved into those few square centimeters of metal.
Here is the raw breakdown of 5 core, high-impact surface decoration technologies for ザマック製の香水キャップ—and how to engineer them without costly mistakes.
The most direct way to execute a logo is right inside the die-casting mold during the primary casting stage.
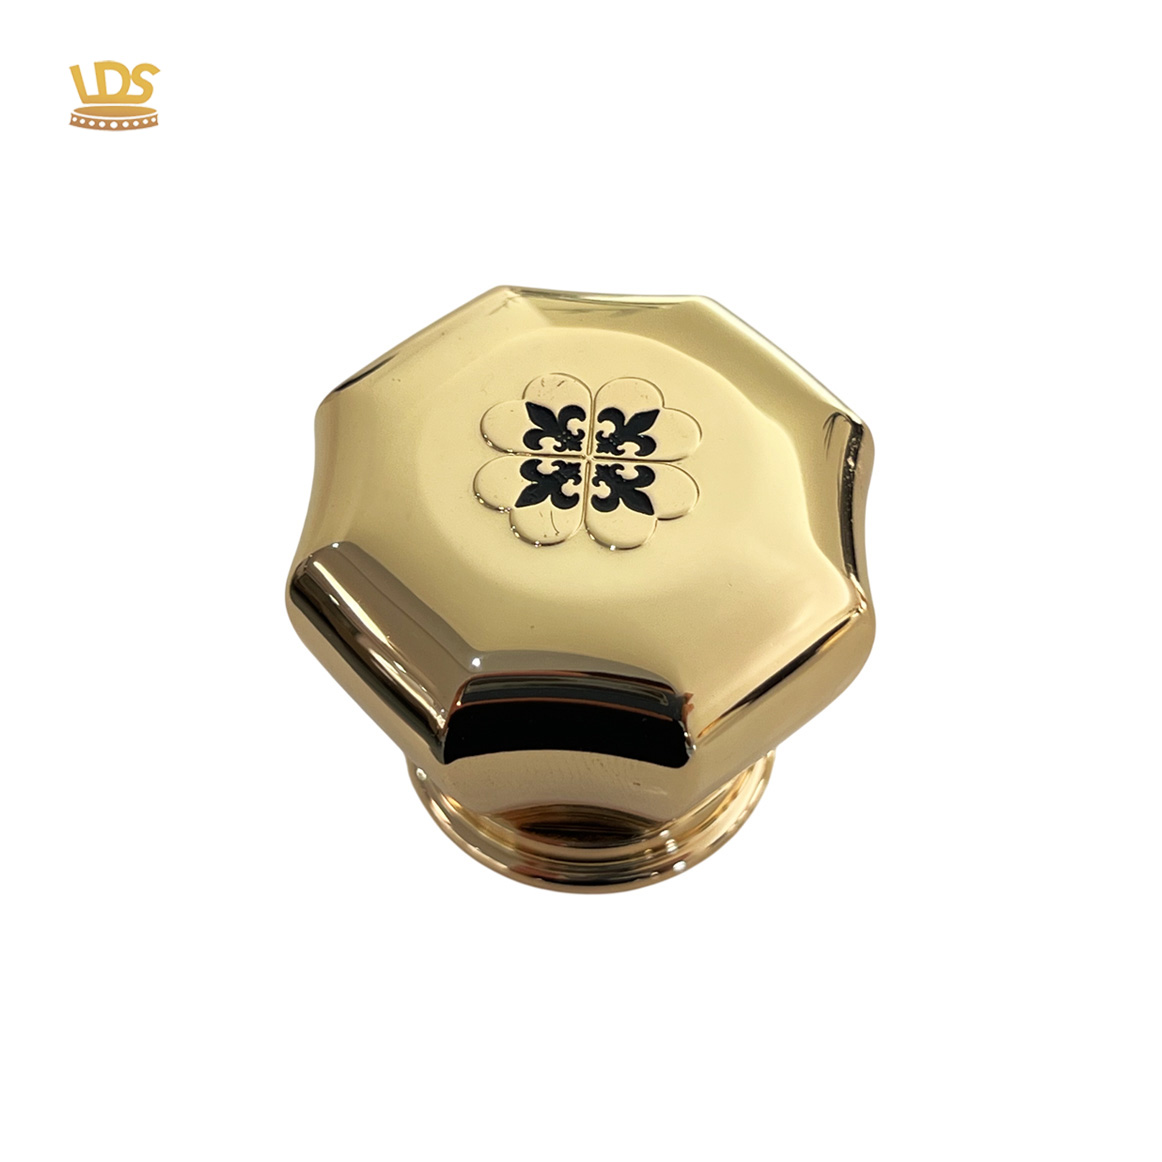
Debossed Logos : Recessed below the surface. Subtly understated, leaving perfect structural pockets for secondary fills like lacquer or epoxy resin.
Embossed Logos : Raised above the surface. Highly tactile with sharp visual contrast and instant sensory feedback.
Designers often draw crisp CAD renders but forget draft angles, or they leave the sharp edges of a 3D logo completely dead-ended. The molten Zamak chokes during cavity filling, and the component tears during ejection.
To hit crisp perfection, starting with high-purity Zamak 3 alloy is non-negotiable. More importantly, mold inserts must be cut using High-Speed CNC or Mirror EDM (Electrical Discharge Machining). Keep embossed heights strictly between 0.3 mm そして 0.5 mm—anything higher looks crude, anything lower feels flat to the touch.
If your fragrance line features limited edition serial numbers, personalized names, or hyper-intricate geometric lines, cutting a custom mold insert for every unit makes zero financial sense. Laser engraving is your problem solver.
It requires no physical contact, utilizing high-energy laser beams to vaporize surface metal or alter thin-film oxide layers with pinpoint accuracy.
Zero-Tooling Customization: Variable data, personalization, and short runs happen seamlessly on the fly.
Ultra-Clean Edges: Achieves line widths as fine as 0.1mm, delivering clarity with surgical-grade precision.
Pro Tip from the Floor:
Laser engraving hits hardest on matte electroplated または PVD-coated surfaces. Vaporizing a dark gunmetal coating to reveal a bright chrome logo underneath delivers a sharp, technical contrast that instantly elevates perceived value.
Need your exact brand Pantone—like iconic turquoise or equestrian orange—embedded into cold metal?
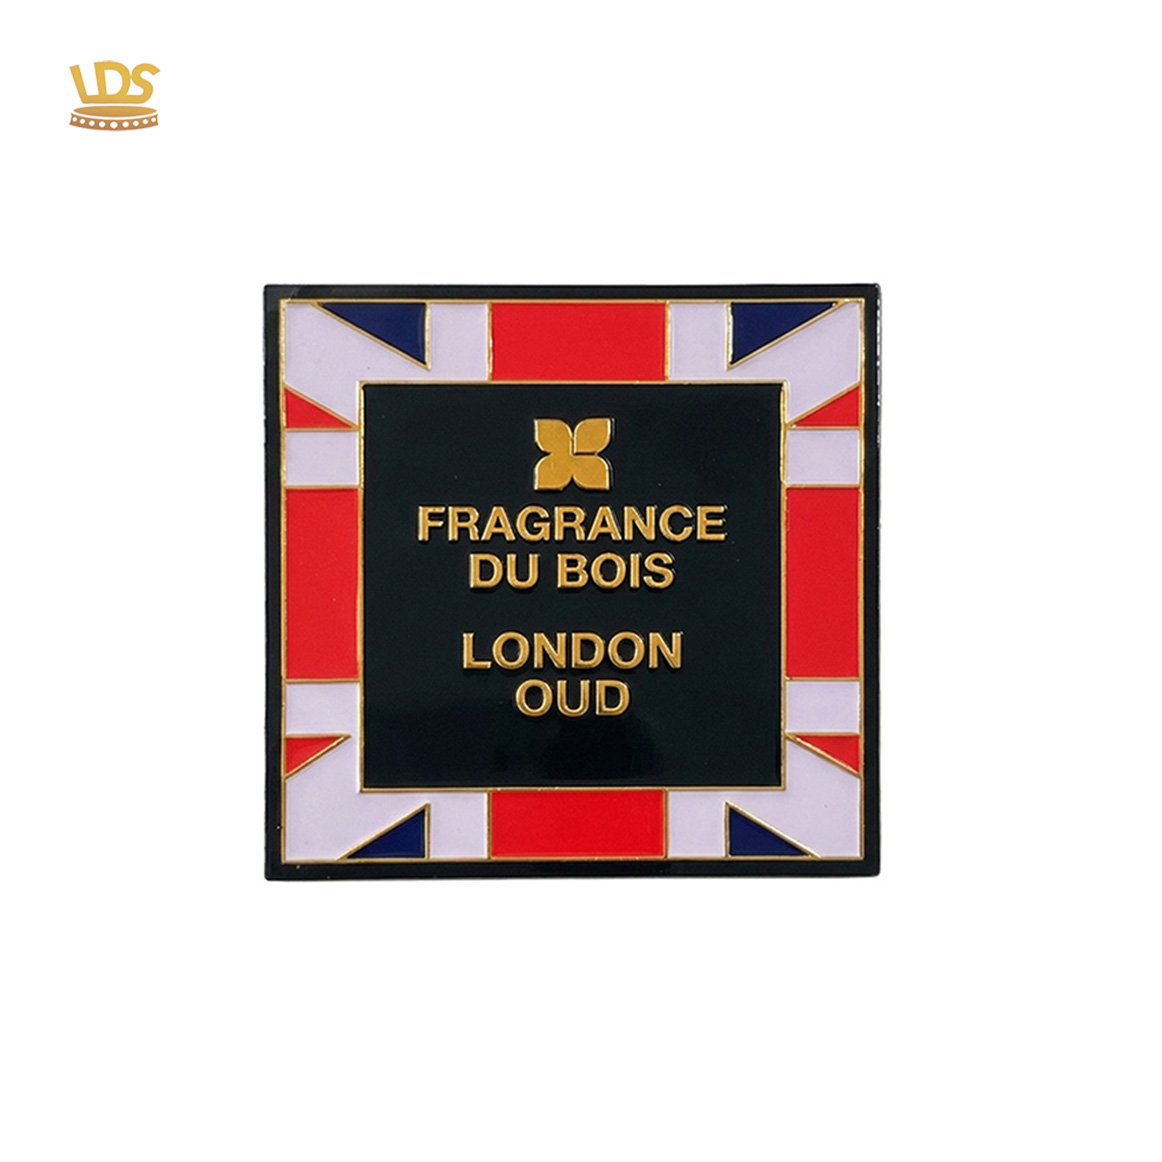
Enamel infill is a staple across high-end niche perfume houses. The process is clean: die-cast a recessed logo cavity into the ザマックキャップ, precision-dispense resin or ink into the channel using micro-droplet nozzles, and heat-cure to set.
Surface Tension Control: Does the cured resin sit flush, concave, or domed (epoxy cabochon effect)? That depends entirely on liquid viscosity and oven temperature ramp rates.
Adhesion Testing: If degreasing fails post-plating, whole chunks of lacquer will pop out after two months on the retail shelf.
It’s all about material contrast—cold, heavy metal framing deep, glossy, high-saturation color.
Examine a €300 niche fragrance bottle and you’ll often find a distinct brass or Zamak plaque inlaid into the top or face of the cap.
This goes way beyond basic surface decorating. This is structural assembly.
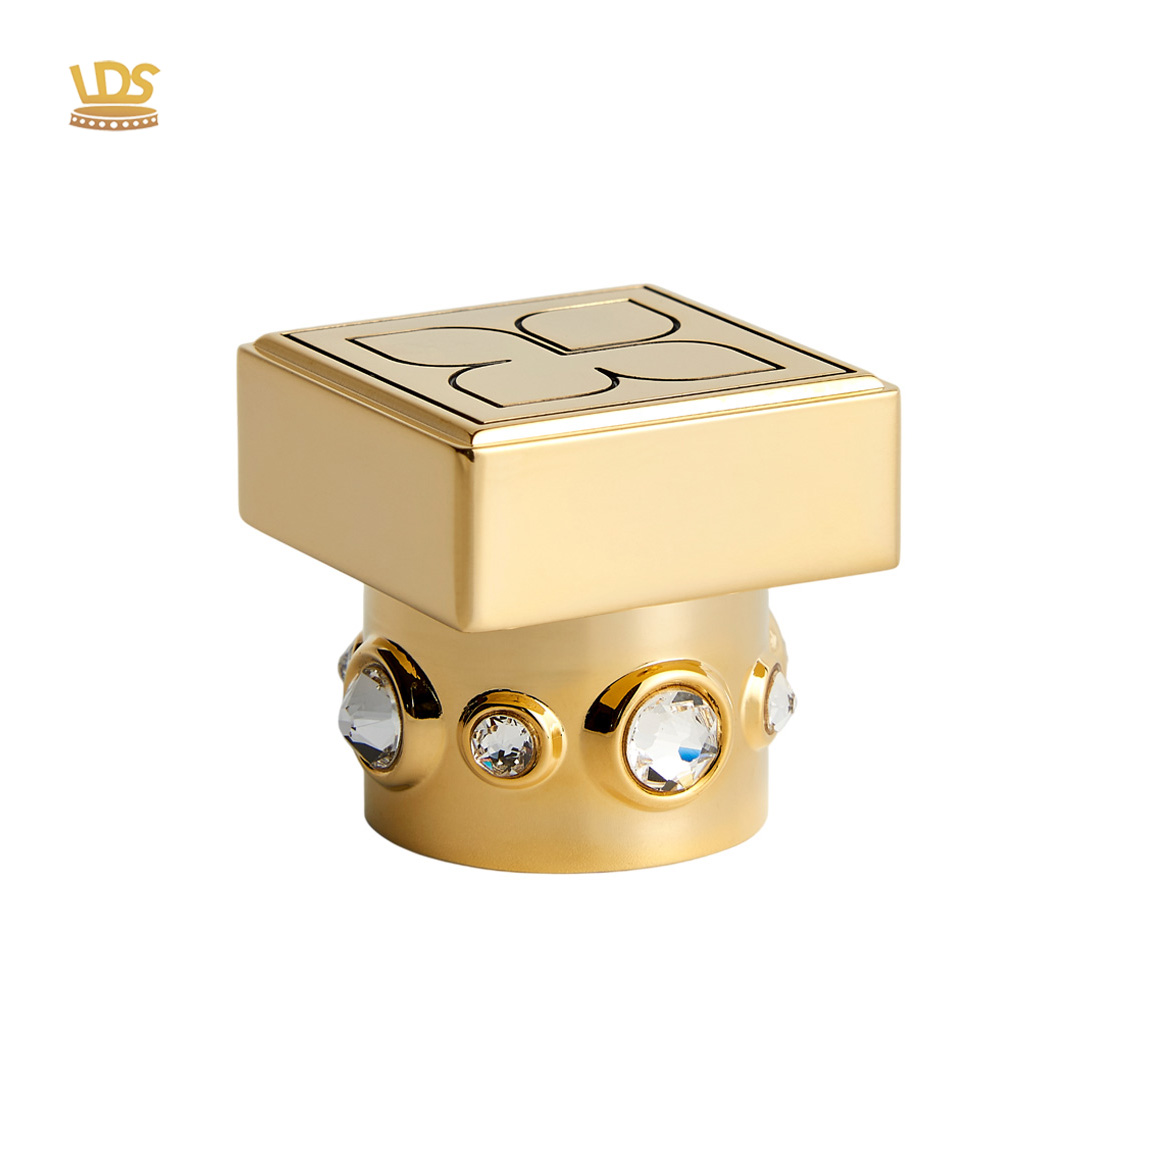
The main cap body is cast or CNC-milled with a designated recess. A separate metal plaque is stamped, electroplated, or hand-patinated (like vintage antique bronze), then bonded into the cavity using industrial-grade structural adhesives or high-tack backing like 3M 300LSE.
Double Tooling & Processing: You are manufacturing two distinct precision metal components instead of one.
Brutal Tolerances: The gap between the recessed pocket and the inlaid plate must stay under 0.1 mm. Too loose and it traps dust; too tight and it won’t seat properly.
When done right, that layered architectural depth is impossible to replicate with single-piece casting or flat printing.
Electroplating acts as your cap’s skin. It dictates whether your logo pops or gets washed out.
Two gold caps can look completely different: one looks like cheap spray-painted plastic, while the other looks like solid 18K gold. The difference comes down to pre-plating polishing and deposit thickness.
Hand Mirror Polishing: Out of the mold, Zamak caps require multi-stage manual polishing to erase part lines, pitting, and micro-air pockets.
Rack Plating (Not Barrel Plating): Individual rack hanging prevents parts from clashing, ensuring uniform plating thickness across complex logo geometry.
Luxury Spec: Apply a gunmetal PVD (Physical Vapor Deposition) coating over polished Zamak, paired with a localized mirror-chrome logo. That depth of reflection speaks for itself on the counter.
A1: リーダーたち Hardware operates a comprehensive 6,000-square-meter industrial production facility. Our capabilities include in-house mold design, high-precision zinc alloy die-casting (utilizing machines ranging from 30 to 168 tons), and multi-stage polishing processes. We specialize in providing end-to-end OEM/ODM solutions—covering everything from 3D design validation and precision mold manufacturing to surface finishing, electroplating, and the assembly of custom interior inserts (made from ABS/PP materials or featuring magnetic structures).
A2: We primarily utilize Zamak 3 (and Zamak 5) for its superior density, structural integrity, and exceptional finishing response. Depending on your brand aesthetic, we offer 5 core logo and decoration tech:
Embossed & Debossed logos directly integrated into the mold.
Micron-level Laser Engraving for variable serial numbers or intricate patterns.
Enamel Infill & Epoxy Resin for exact Pantone color matching.
3D Metal Plate Inlays utilizing high-tack 3M 300LSE structural adhesive.
Real Precious Metal Plating & PVD Coatings (such as matte gunmetal, 18K gold, or mirror chrome).
A3: During the preliminary CAD design phase, our mold engineers rigorously optimize the draft angles. We employ high-speed CNC machining and mirror-finish electrical discharge machining (EDM) to produce the inserts for logos, keeping the relief height between 0.3 and 0.5 mm. This ensures optimal flow of the molten zinc alloy, facilitates smooth demolding, and results in crisp, well-defined edges.


コメントを残す